Sensor solutions for continuous conveyors in intralogistics
So-called continuous conveyors are a proven solution for in-house material flow. These include, in particular, conveyor belts, roller conveyors and chain conveyors, which continuously move load carriers and objects along predetermined transport routes. They are incorporated into the planning and design of storage and production systems from the outset, connecting the various functional areas.
The selection of the appropriate conveyor system depends primarily on the transported goods’ dimensions, weight and features. Robust chain and roller conveyors are predominantly used for pallet conveying. For cartons, trays, and containers, on the other hand, conveyor belts and roller conveyors with appropriately sized rollers are often suitable. This allows the transport system to be tailored specifically to the respective transport requirements and process flows.
Sensor technology along continuous conveyors
Continuous conveyors ensure a continuous material flow and are an essential component of transport systems in both flow production and goods distribution centers. The selection of the appropriate system depends primarily on the type, dimensions, and weight of the goods to be transported. Conveyor belts and link-belt conveyors, for example, are suitable for individual items and cartons, while roller and chain conveyors are primarily used for containers, pallets, and large, heavy transport units. In addition, continuous conveyors are used to connect automated warehouses, particularly for storage and retrieval, as well as for the entry and exit of loading units.
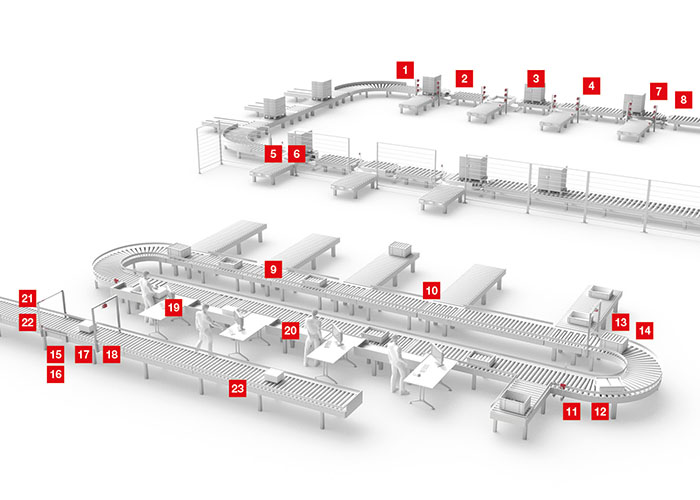
Click on the numbered applications to learn more about the respective sensor solutions.
Continuous conveyors for different load carriers
The type of load carrier determines both the design of the transport system – including roller diameter and spacing – and the requirements for the sensor technology used. For clarity, the following sensor applications are therefore organized by load carrier type.
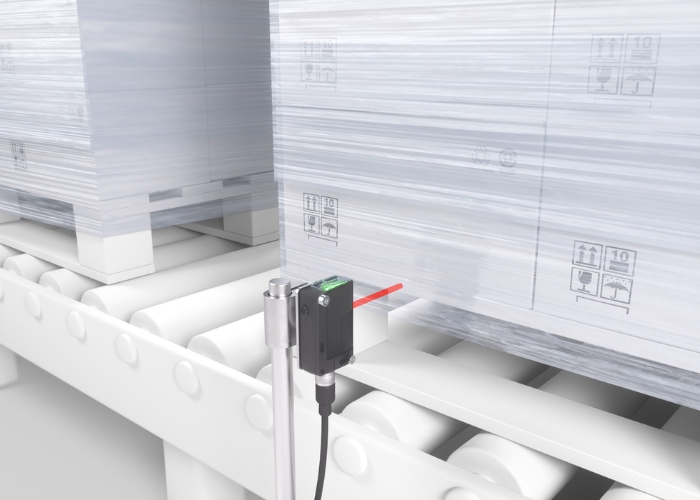
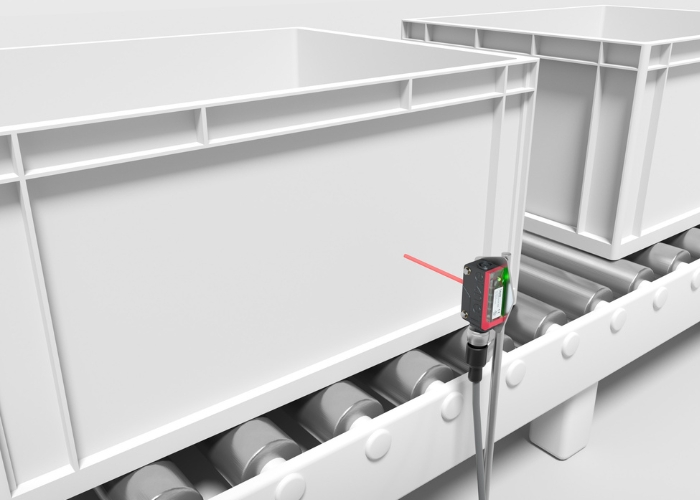
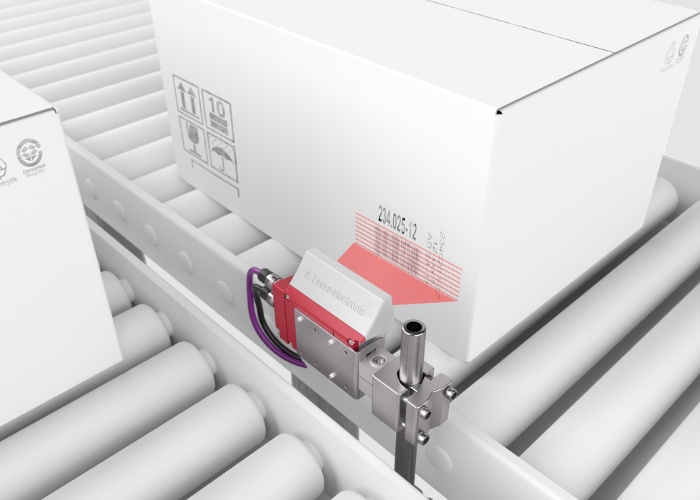

Applications in pallet conveying
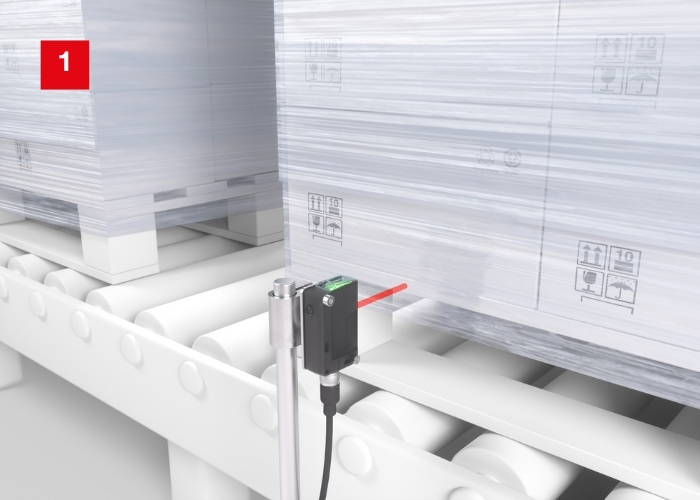
Detection of shrink-wrapped pallets
Requirement:
The film- or shrink-wrapped pallets must be reliably detected over their entire length. The output signal of the sensor used must not show any fluctuations.
Solution:
The PRK 46C.D and PRK 25C.D retro-reflective photoelectric sensors are optimized for use on roller conveyors. They offer high functional reliability especially for film- and shrink-wrapped pallets. Thus, the sensor generates a stable output signal as long as the object is within the detection range.
Detection of pallets
Requirement:
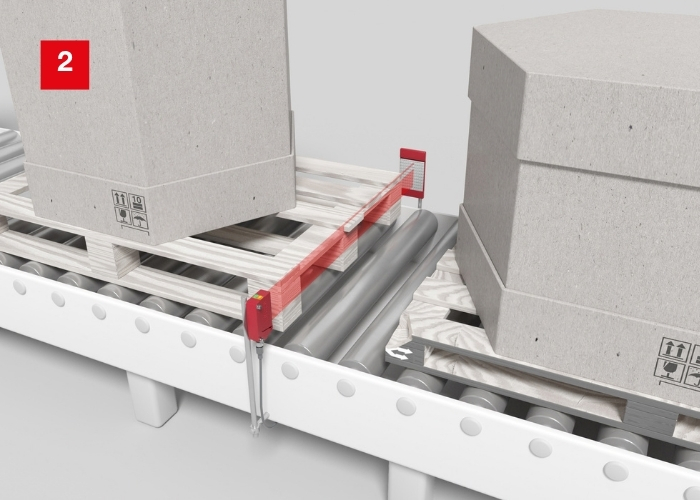
All types of pallets must be reliably detected along their entire length. Defective pallets or openings on pallets must also be permitted.
Solution:
The PRK 46C retro-reflective photoelectric sensors also reliably detect objects with irregular shapes and openings. For this purpose, the devices use a powerful, 60 mm wide light-band.
Detection of pallets from below
Requirement:
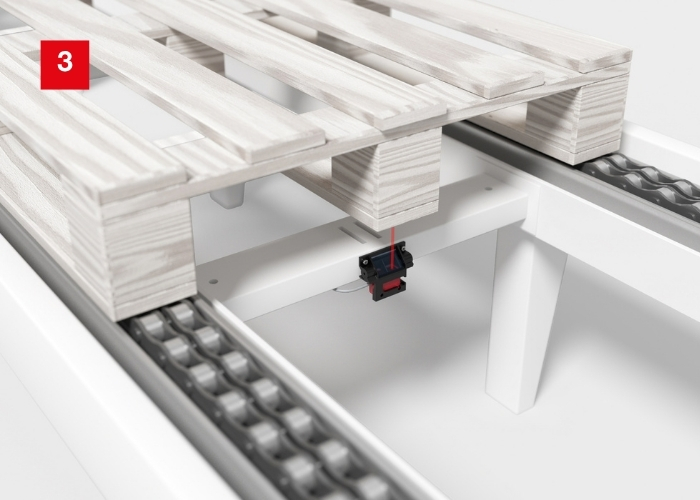
Different types of pallets run over a conveyor system, which must be reliably detected from below. High-frequency hall lighting and dirt particles must not affect the sensor. In addition, the sensors should not require any additional work during the installation of the conveyor line.
Solution:
The HT 25C series diffuse sensorscan be mounted by the transport system manufacturer in the interior of the conveyor by means of a special holder. This has an integrated front screen for the discharge of dirt particles. The special ambient light parameterization of the sensors efficiently suppresses ambient light sources.
Width and height verification
Requirement:
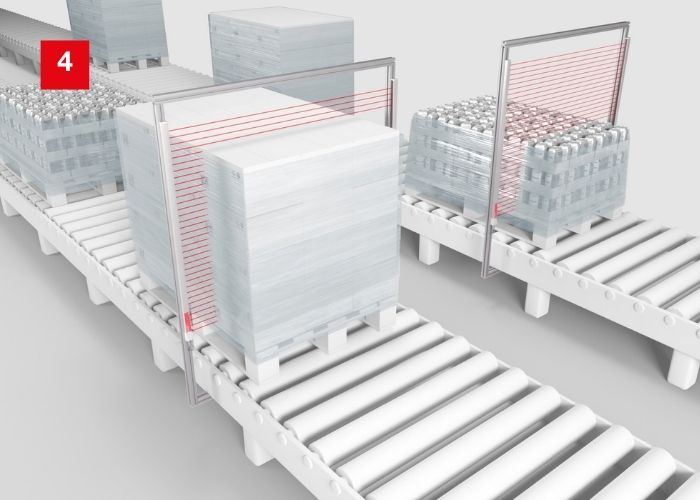
Before a pallet can be fed into the transport system or storage system, the dimensions of the loaded pallet must be checked.
Solution:
The CSL 710 switching light curtains check the dimensions of the loaded pallet. Different resolutions and measuring field lengths as well as 4 configurable inputs / outputs allow the devices to be optimally adapted to the application and easily aligned thanks to the integrated display.
Access guarding with muting
Requirement:
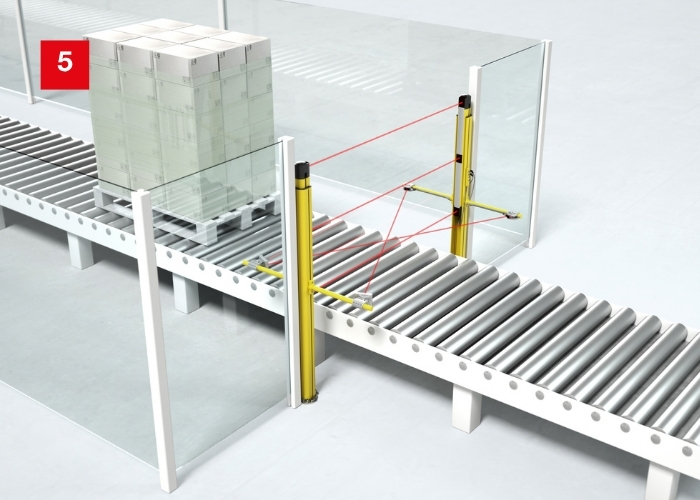
Access guarding on the conveyor line is to prevent persons from accessing the dangerous areas, while at the same time allowing the transported goods to pass through.
Solution:
The muting function bridges the safety sensor in a controlled manner to allow the transported goods to pass through. This function is already integrated in the MLD 300 or MLD 500 multiple light beam optical safety sensors and the MLC 500 safety light curtains.
> Read more about multiple light beam optical safety sensors
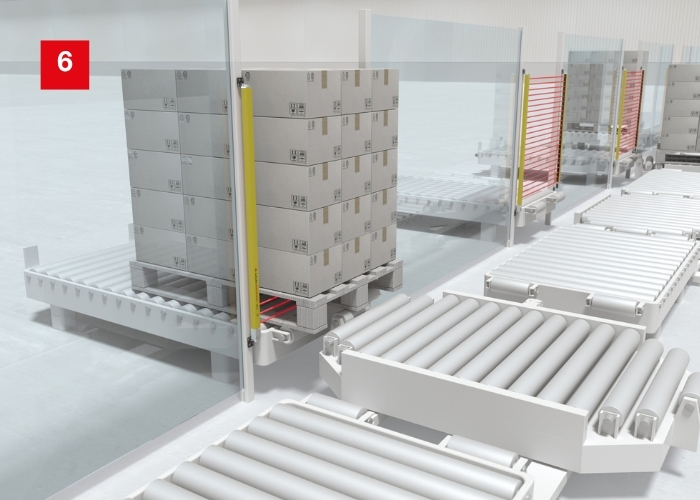
Access guarding with Smart Process Gating
Requirement:
Access guarding on the conveyor line is to prevent persons from accessing the dangerous areas, while at the same time allowing the transported goods to pass through. At the same time, the safety technology should take up as little space as possible.
Solution:
With Smart Process Gating, the safety sensor is bridged by means of a control signal from the PLC. The function is integrated in the MLC 530 SPG safety light curtain. Additional muting sensors are no longer required, and particularly space-saving systems can be designed thanks to SPG.
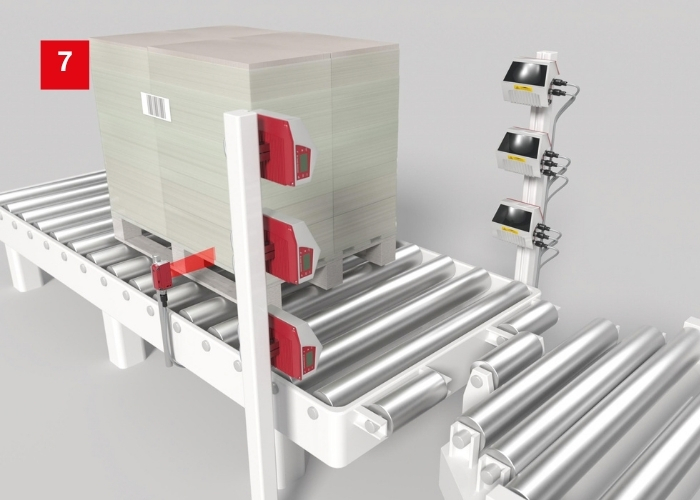
Code reading on the pallet
Requirement:
During goods receipt or shipping, the goods code should be read in and transferred to the higher-level system. The position of the label can vary.
Solution:
Several bar code readers of the BCL 500i / BCL 600i series are used to read the code label in varying positions. Using the integrated switch, the devices can be connected both to each other and directly to the control system via a line structure.
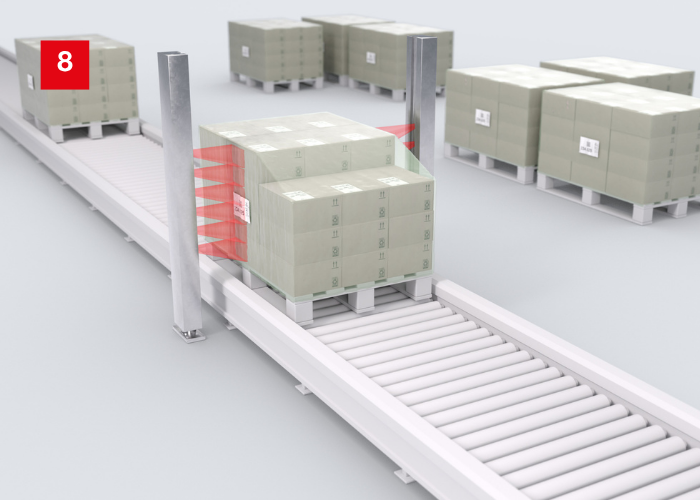
Efficient goods receipt
Requirement:
In the incoming goods area, 1D- and 2D-codes on pallets are to be detected automatically from both sides. Identification must be reliable regardless of code quality and label type. In addition, intelligent data preprocessing with duplicate detection and filtering, as well as rapid error analysis, are required.
Solution:
The scanGATE solution combines global-shutter cameras, high-performance LED illumination, and intelligent software into one comprehensive identification system. Functions such as duplicate detection, data filtering, and a ring memory enable transparent data capture and rapid error analysis. The scalable system automates pallet identification, reduces errors, and can be integrated into existing logistics and IT processes.
Applications in container and tray conveying
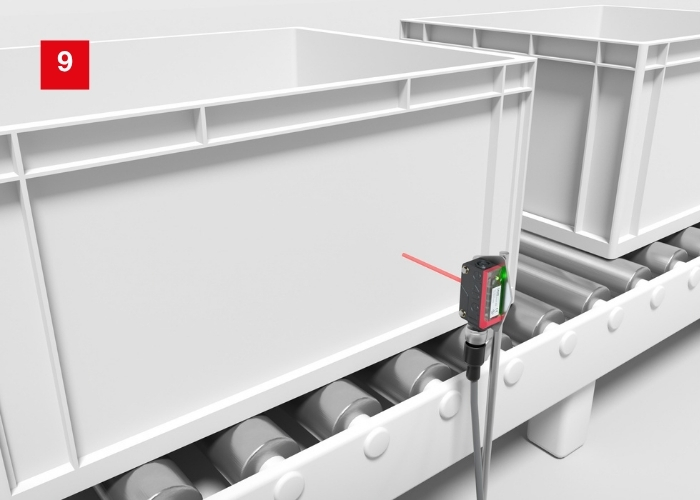
Detection of containers and trays
Requirement:
A container or tray should be reliably detected as it passes by. The sensors used should be easy to mount and connect.
Solution:
With their compact cubic design, the 5 series optical sensors are used for powerful and cost-optimized standard detection tasks. The integrated M3 metal threaded sleeves and the flexible cable outlet downwards or to the rear simplify installation even in situations with limited installation space.
> Read more about diffuse sensors with background suppression
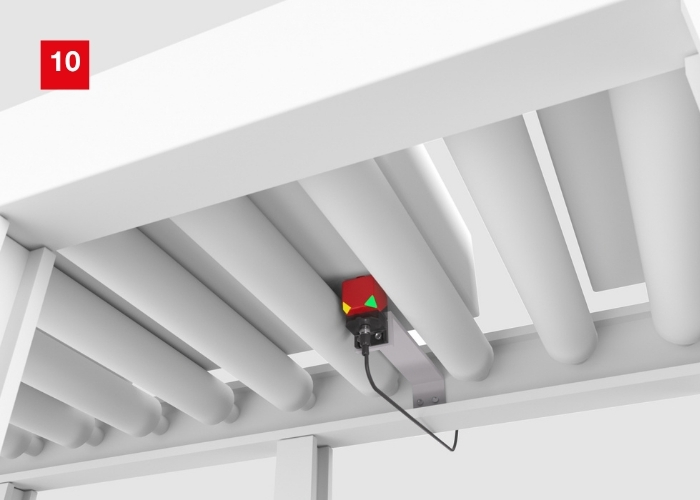
Detection of the closing state of flaps
Requirement:
To stop the containers, the closing state of the flap must be checked.
Solution:
The IS 244 series inductive sensors detect the closing state of the flap. Versions with M12 connector or comfortable terminal compartment are available for the connection.
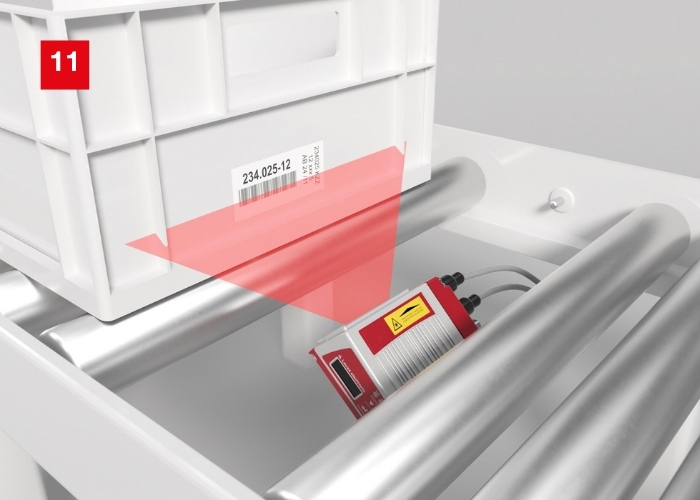
Code reading on containers and trays
Requirement:
The bar codes attached to the containers or trays should be read and the information transferred to the control via a fieldbus. It must also be possible to mount the code reader between conveyor lines.
Solution:
The bar code readers of the BCL 200i and BCL 300i series can be mounted at a short distance from the code due to their minimal reading distance of only 40 and 20 mm. With its integrated switch, line structures can be set up in all Ethernet-based fieldbuses. The parameters are set via the control.
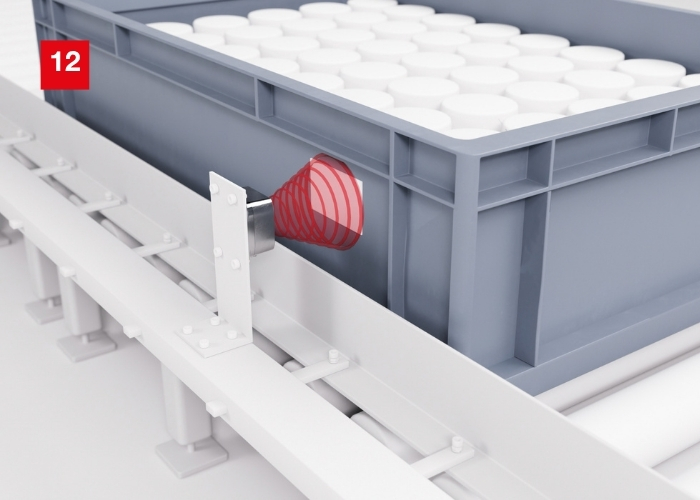
Identification of containers on a conveyor line
Requirement:
In the material flow, containers are automatically transported to the desired destinations. For this purpose, the containers and their contents must be reliably identified at loading, transfer or distribution stations as well as in the warehouse.
Solution:
RFID can be used to solve identification tasks when bar code labels are not reliably readable, e.g. due to increasing soiling of the containers or regularly required cleaning processes. The RDH 202/242 RFID read/write device can reliably read containers with RFID tags in a fixed position and at a defined reading distance – even dynamically. When using so-called onMetal tags, it can also read metal containers.
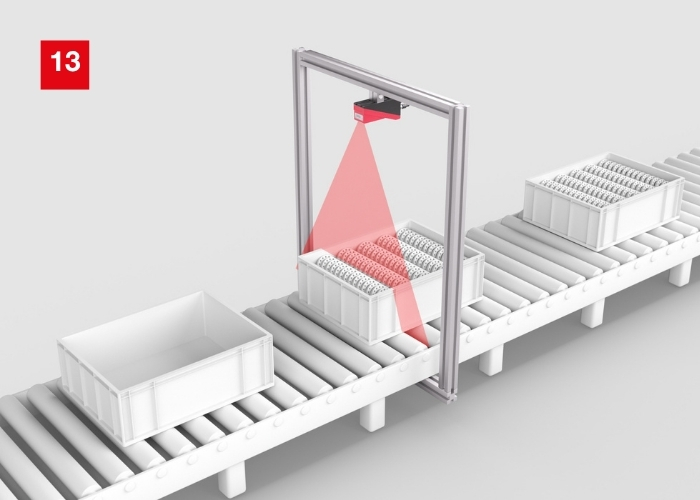
Check for residual contents in the container or empty container check
Requirement:
To use a container again, it must be checked whether there are still objects in the container.
Solution:
The LRS 36 light section sensors use a laser line for sensing object detection. Thus, the presence of objects in the container can be reliably determined.
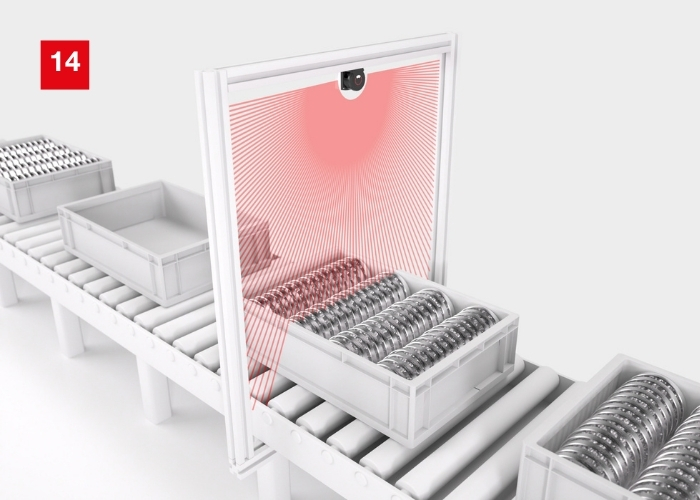
Container content check
Requirement:
To ensure uninterrupted operation, care must be taken when filling containers to ensure uniform distribution, proper alignment with the outer edges, and the detection of empty containers.
Solution:
The configurable detection ranges of the measuring laser scanner ROD 300 and switching laser scanner ROD 100 allow monitoring windows to be set up, within which objects are reliably detected. If specified detection criteria are violated, a switching output can trigger the ejection of the affected container.
Applications in carton and polybag transport
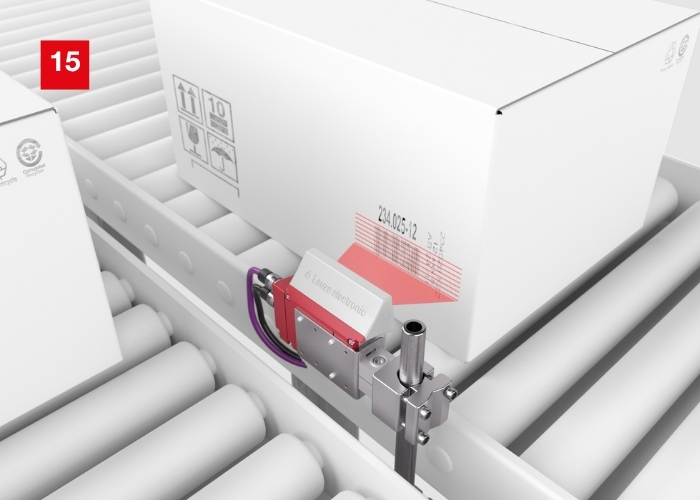
Code reading of codes printed directly on the carton
Requirement:
A bar code printed directly on the carton must be read. The read information must then be transferred to a control.
Solution:
The BCL 300i series bar code readers feature specialized optics for reliable detection of inkjet-printed bar codes on cartons. The integrated switch allows the devices to be easily integrated into linear Ethernet network structures. They can be configured centrally via the higher-level control.
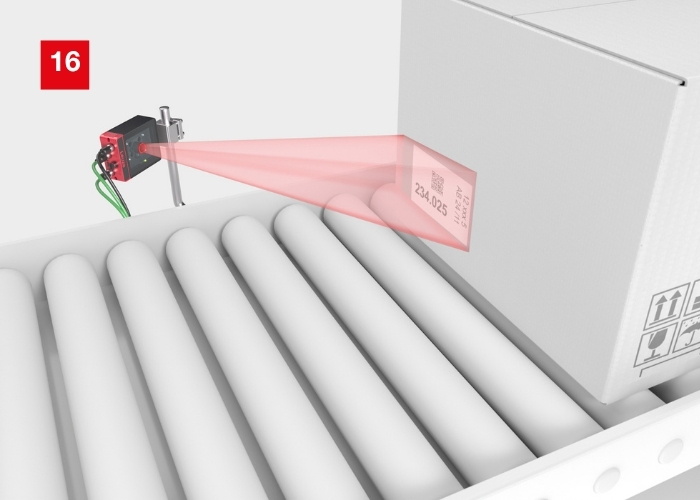
Angled bar code reading from the side in carton and container transport systems
Requirement:
In many intralogistics applications, bar codes are arranged in a ladder or picket fence pattern on the front or rear side of cardboard boxes and containers. To ensure reliable identification, these codes must be captured accurately while the objects pass through the reading station, sometimes at high speed. Often, only a side view of the conveyor line is available.
Solution:
The camera-based code reader DCR 300i enables reliable code capture even from oblique side angles. Thanks to its camera-based technology, barcodes are reliably identified regardless of their orientation – whether in ladder or picket fence arrangements. Combined with long-range optics, the DCR 300i offers highly flexible reader positioning and enables reliable detection even at greater working distances. This simplifies integration into existing conveyor systems and ensures a high reading rate across a wide variety of applications.
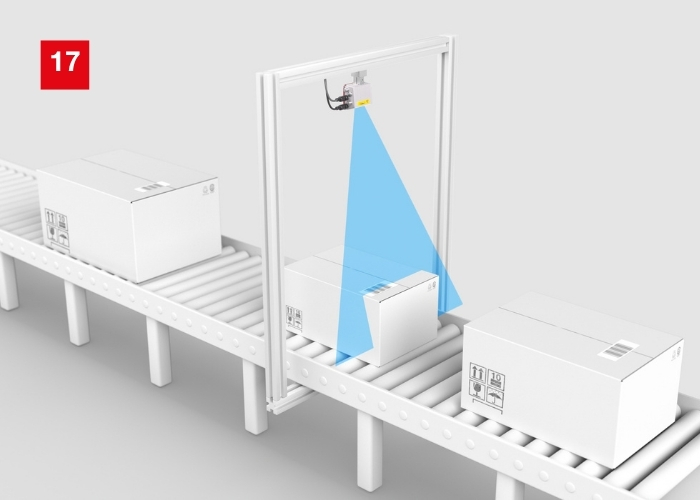
Code reading on the top of aligned cartons
Requirement:
When goods are dispatched from mail order and e-commerce, the bar code on the shipping labels must be read. The aligned cartons usually differ significantly in their dimensions. The read information must be transferred to a control.
Solution:
The BCL 600i series bar code readers read the codes on cartons from above. They work with blue laser light for more depth of field at small modulus widths and thus do not require expensive focus adjustment. The devices can be easily integrated into the control via the integrated fieldbus interfaces.
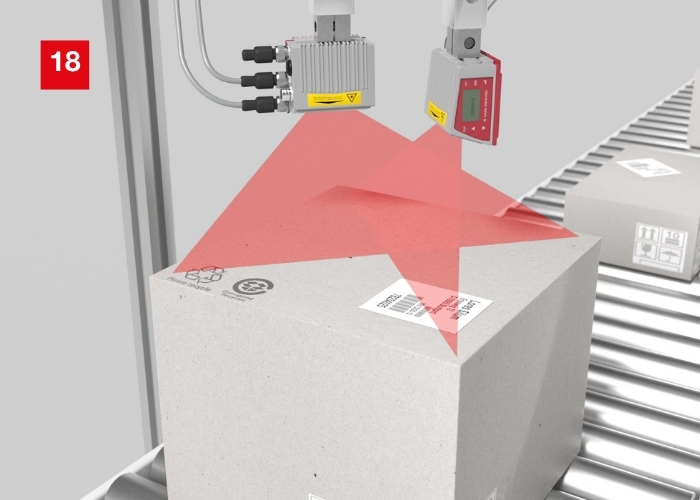
Code reading on the top of unaligned cartons
Requirement:
When goods are dispatched from mail order and e-commerce, the bar code on the shipping labels must be read. In this case, the non-guided cartons usually differ significantly in their dimensions and orientation. The read information must be transferred to a control.
Solution:
The modular scanner portal MSPi combines at least two coordinated bar code readers to reliably capture bar codes regardless of their orientation. Application-specific portal solutions are also available to meet specific requirements. Thanks to the integrated fieldbus interface, the scanner portals can be easily integrated into the higher-level system control.
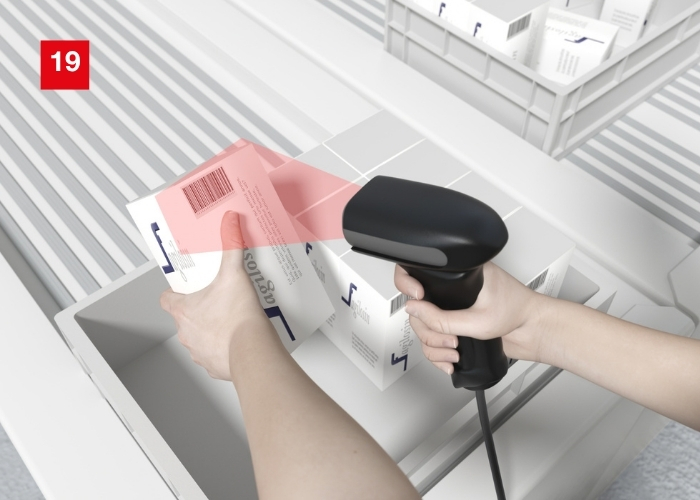
Manual code reading
Requirement:
During order picking, the goods codes must be read and transferred to the goods management system.
Solution:
The IT 1472Xg series mobile bar code readers read all bar codes commonly used in warehousing and logistics. Depending on the application, versions with cable connection or radio transmission are available.
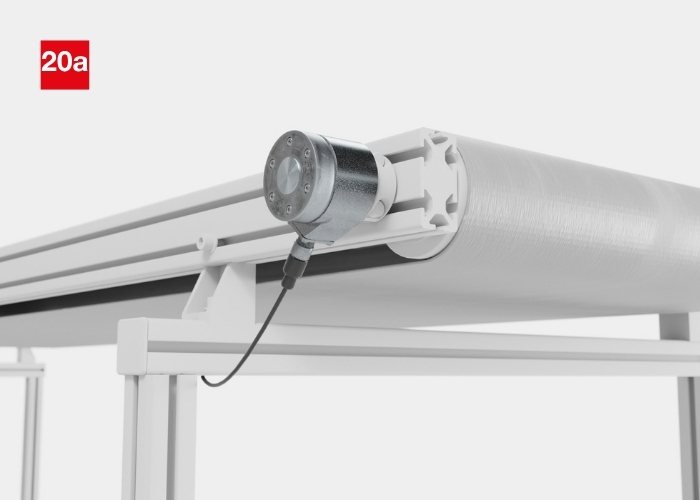
Conveyor belt speed monitoring
Requirement:
In storage systems and material flow technology, rotary encoders play a key role in monitoring conveyor belts and other continuously operating transport systems. By reliably measuring rotational movement and speed, they help monitor proper operation and ensure system availability. At the same time, they detect operating conditions such as idle mode and use this information to specifically reduce energy consumption. The measurement is to be performed using a sensor that monitors the rotational movement directly on a conveyor roller.
Solution:
An EI series rotary encoder can be flexibly mounted directly on a conveyor roller to reliably measure rotational movement and speed and provide this data for system control. Various resolutions and interfaces are available depending on requirements.
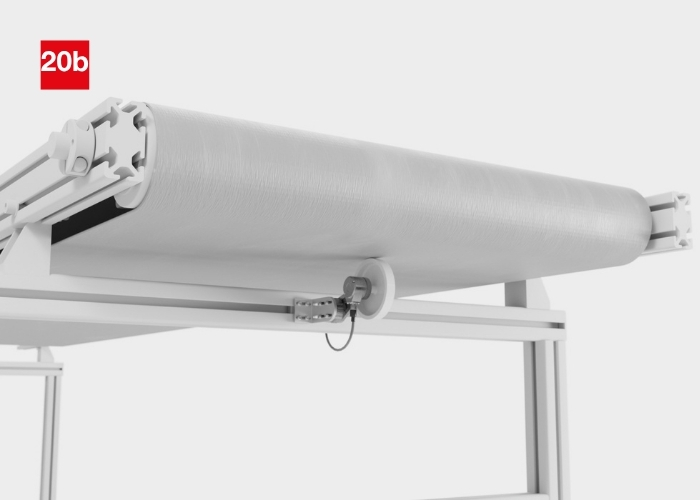
Detection of rotational motion
Requirement:
The reliable measurement of rotational motion and speed helps monitor proper operation and ensure the transport system’s availability. Direct integration onto the drive roller is not always possible.
Solution:
An EI series rotary encoder with a roller wheel can be flexibly mounted directly on or below the conveyor belt to detect rotational movement and speed and transmit this data to the control. Various resolutions and interfaces are available depending on requirements.
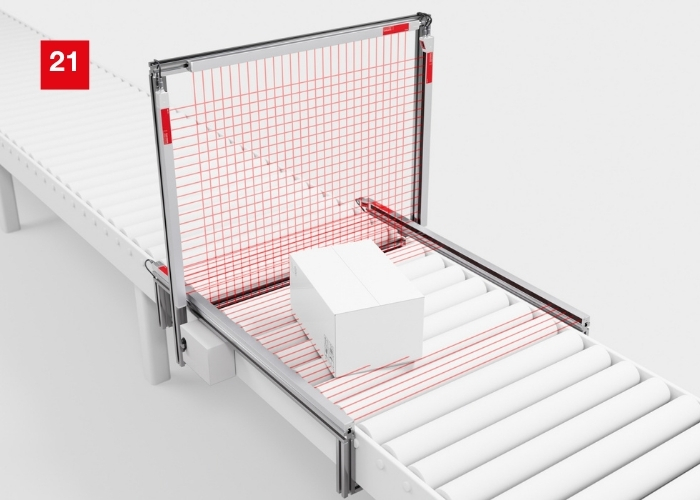
Contour check and volume calculation for cartons
Requirement:
The carton transported on the transport system is to be gripped automatically for palletizing. In another application, it should be detected whether the carton is intact and closed. For both applications, the contour of the carton must be checked.
Solution:
The CMS 700i 3D contour measurement system detects the length, width, height, protrusions, deformations and position of any objects as they pass by, independent of their shape and surface structure. Even polybags are reliably detected. The complete system contains all components required for installation and operation.
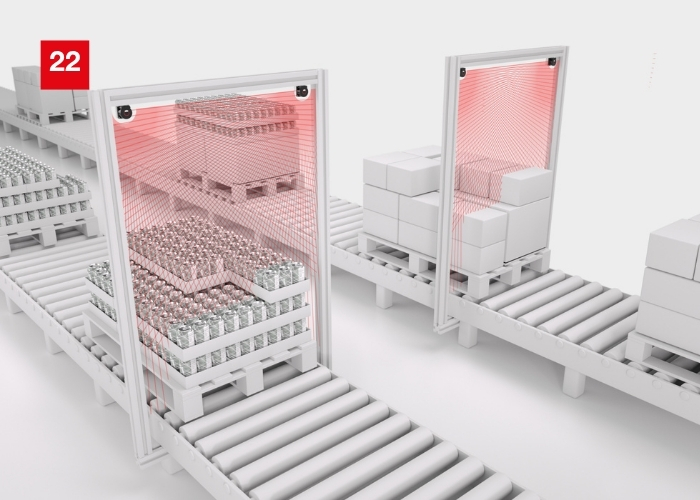
Volume measurement solution
Requirement:
In a warehouse, goods are to be measured precisely and reliably on continuous conveyors or AGVs during transport. This involves recording length, width, height, and contour, as well as detecting protrusions, bulges, and defects. In addition, the system must be able to integrate flexibly into existing automation and logistics processes.
Solution:
The volumeGATE volume measurement system detects goods in three dimensions using light grids or laser scanners and determines their volume and contours. It detects protrusions and bulges and enables completeness monitoring of individual layers. Additionally, scales, bar code scanners, or the scanGATE can be integrated for automated pallet identification. The measurement data is transmitted directly to existing customer applications via a central interface such as PROFINET or Ethernet TCP/IP. In this way, volumeGATE achieves greater process reliability and improved data quality in logistics processes.
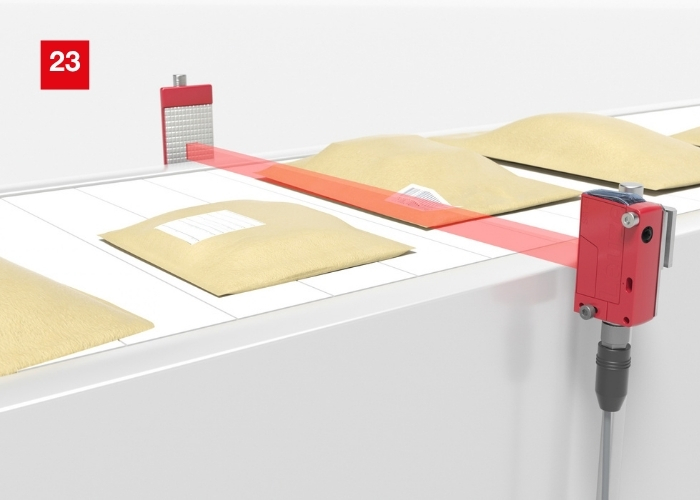
Detection of polybags
Requirement:
Polybags must be reliably detected along their entire length at speeds of up to 2.5 m/s on a belt conveyor.
Solution:
The RK 46C series retro-reflective photoelectric sensors reliably detect objects as small as 5 mm on a belt conveyor system. For this purpose, the devices use a 25 mm wide, powerful light-band. Due to the high switching frequency of 250 Hz, the RK 46C detects objects even at high conveyor speeds.
Challenges and sensor technology for continuous conveyors
The transport system’s type and version play a key role in determining the sensors’ integration options and positioning. To ensure reliable system operation, load carriers such as pallets and containers must be reliably detected, their dimensions and fill levels monitored, and bar codes and other identification codes reliably read. These functions lay the foundation for a transparent material flow and smooth process operations. For extensive conveyor lines in particular, a suitable network infrastructure is essential to efficiently integrate sensors with data output into linear communication networks.
A key strength of continuous conveyors is their high transport capacity. Their modular, segmented design allows for the creation of accumulation sections and crossing points where transport units can be controlled as needed to prevent collisions. Diverting sections also make it possible to remove defective goods or goods requiring inspection from the main flow without significantly disrupting the continuous material flow. The requirements for the sensor system vary depending on the load carrier: In the case of pallets, differences in the condition and quality of exchangeable pallets lead to significant detection variations. Containers, on the other hand, often remain in the logistics system permanently, which generally results in more consistent features and detection conditions.
The extensive sensor portfolio from Leuze enables reliable and fast object detection while also helping to protect people and equipment. Various identification technologies such as bar codes, 2D-codes, and RFID offer flexible solutions for detecting and tracing of goods and load carriers. Even with challenging object characteristics, such as shiny or dark surfaces, as well as highly reflective packaging, powerful sensors ensure reliable detection – even under harsh environmental conditions.
For continuous conveyor manufacturers, easy sensor integration and short commissioning times are key factors in reducing on-site installation effort. Leuze supports this with user-friendly sensor functions, tailored mounting solutions, and easy adjustment. Integration into existing automation structures is further facilitated by suitable fieldbus interfaces, such as PROFINET. This allows sensor solutions to be efficiently installed, configured, and integrated into higher-level control systems.